7 Best Fully Electric Continuous Pyrolysis Plants in 2026
Choosing among the 7 Best Fully Electric Continuous Pyrolysis Plants in 2026 requires more than comparing price and advertised capacity. A serious evaluation examines reactor design, electrical efficiency, feedstock flexibility, temperature stability, product quality, safety systems, and after-sales support. These details decide whether a plant performs steadily or struggles during ordinary production changes.
Professor Ondřej Mašek, a respected biochar and pyrolysis researcher at the University of Edinburgh, offers a useful caution: “Pyrolysis performance depends on feedstock, process conditions, and the intended product.” That principle remains important when reviewing modern Fully Electric Continuous Pyrolysis Plant systems. A clean electrical heater can provide precise thermal control, but it does not remove every engineering challenge. Moisture, particle size, contamination, and uneven feeding can still reduce output.
This guide compares leading plant concepts through a practical, evidence-based lens. It considers real operating details, including power consumption, heating uniformity, continuous feeding, gas handling, maintenance access, and monitoring controls. Some manufacturers publish impressive figures. Those figures deserve verification.
A plant may look efficient on paper.
Actual performance can differ.
Readers should request test data, reference projects, warranty terms, and independent technical documentation before making a decision. The ranking is therefore a useful starting point, not a final verdict. Even advanced electric systems need careful commissioning, trained operators, and realistic feedstock planning. That is where many projects succeed—or quietly lose efficiency.
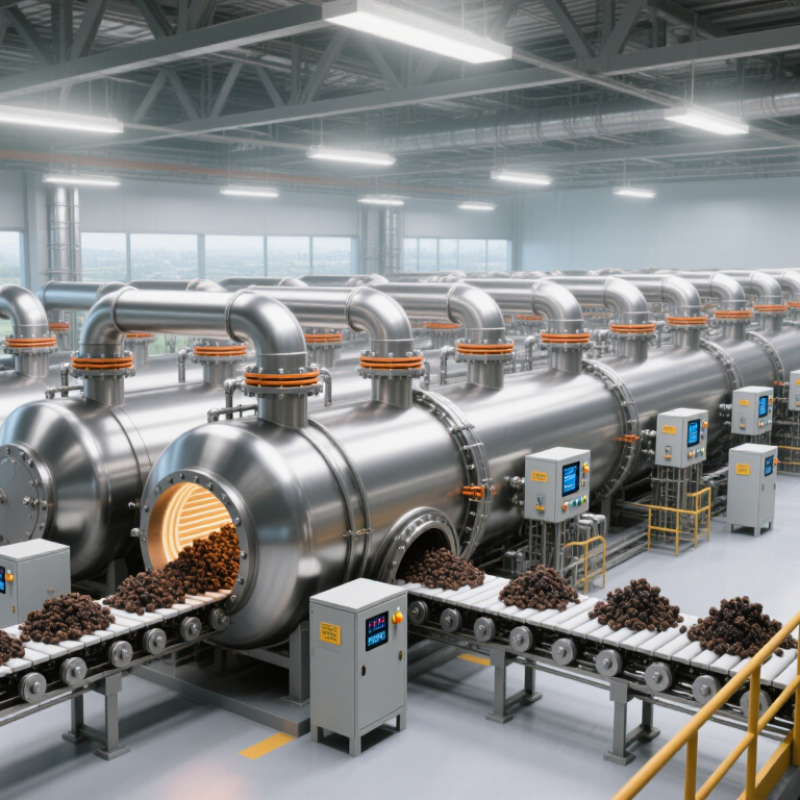
Table of Contents [Hide]
What Fully Electric Continuous Pyrolysis Plants Are
Fully electric continuous pyrolysis plants convert approved carbon-based feedstocks inside a sealed, oxygen-limited reactor. Electric heating supplies process energy instead of burning fuel directly. This design can reduce onsite combustion emissions and improve temperature control.
A continuous system feeds prepared material through the reactor with conveyors, screws, or pumps. Products leave the system without stopping the main heating cycle. Depending on the feedstock, outputs may include pyrolysis gas, liquid fractions, and solid char. Operators monitor reactor temperature, pressure, feed rate, and oxygen levels continuously. Small changes matter. Uneven feedstock can create unstable heating and inconsistent product quality.
In practical operation
In practical operation, the plant needs shredders, dryers, condensers, gas treatment, sensors, and emergency controls. Electric heating does not make the process automatically clean or risk-free. Electricity may still come from carbon-intensive sources, and exhaust treatment remains important. Proper permits, feedstock testing, fire protection, and worker training are essential. From an engineering perspective, the strongest systems balance energy efficiency with reliable maintenance access. Some designs appear impressive on paper but struggle with sticky materials, moisture, or unexpected contaminants. That limitation deserves honest attention. Experienced operators therefore test feedstock before scaling production and record performance under changing conditions.
How Electric Continuous Pyrolysis Technology Works
Fully electric continuous pyrolysis plants heat feedstock without direct combustion inside the reactor. Electrical elements transfer controlled heat through reactor walls or internal heating zones. A screw or conveyor moves prepared material at a steady rate. With limited oxygen, the feedstock separates into gas, liquid, and solid char.
Temperature sensors track several heating sections continuously. The control system adjusts power when moisture or particle size changes. This matters because uneven feedstock can create cold spots, sticky deposits, or unstable output. Recovered process gas may support heating, but electric systems still require reliable grid capacity. Proper insulation also reduces heat loss and protects nearby equipment.
Tips: Dry the feedstock before testing. Keep particle size consistent. Record temperature, residence time, and product moisture during each run. Check emergency shutdowns regularly. Do not trust one sensor alone. Independent laboratory testing can verify char quality and liquid composition. Engineering practice suggests starting slowly, although production pressure often encourages the opposite. That shortcut deserves reconsideration. A well-designed plant should provide clear maintenance access, documented operating limits, and measured emissions data. Safety depends on disciplined operation, not electricity alone.
Key Criteria for Evaluating the Seven Best Plants
Evaluating the seven best fully electric continuous pyrolysis plants requires more than comparing processing capacity. A reliable review begins with feedstock flexibility, thermal stability, and verified operating data. Inspectors should examine how evenly electric heaters distribute heat across the reactor. Cold zones can reduce product quality and increase maintenance needs. Continuous feeding also matters. A stable screw or conveyor system should prevent bridging, leakage, and sudden pressure changes. Operators should provide records from extended trials, not only short demonstrations.
Energy efficiency deserves careful attention. Compare electricity consumption per tonne of approved feedstock, including heating, feeding, cooling, and gas treatment. Safety systems should include temperature sensors, pressure relief equipment, emergency shutdowns, and documented inspection routines. Emission controls must match local permits and measured output. Independent laboratory testing adds credibility. However, laboratory results can vary with moisture, particle size, and feedstock composition. That limitation should be stated clearly.
Tips: Request a complete mass-and-energy balance. Ask for twelve months of maintenance records. Visit an operating site, if possible. Watch the control room during startup and shutdown. Speak with operators, not only sales staff. I would also compare warranty terms carefully. A long warranty means little without spare-part availability and trained service support. No plant is perfect. The strongest choice is the one with transparent weaknesses, repeatable performance, and evidence that matches its claims.
7 Best Fully Electric Continuous Pyrolysis Plants in 2026
Key Criteria for Evaluating the Seven Best Plants
This screening model uses a 100-point weighted framework for comparing seven fully electric continuous pyrolysis plants. The highest priority is given to verified throughput and energy performance, followed by continuous operating stability, feedstock flexibility, emissions control, product quality, and process safety. Scores should be validated against third-party test reports, operating records, energy meters, emissions measurements, and applicable safety standards before procurement.
Seven Leading Fully Electric Continuous Pyrolysis Plants in 2026
In 2026, the seven leading fully electric continuous pyrolysis plants reflect different heating and reactor strategies. They include electrically heated rotary kilns, twin-screw reactors, fluidized-bed units, vertical shaft reactors, induction-heated chambers, microwave-assisted systems, and modular conveyor reactors. Each design aims to maintain stable temperatures without direct fossil-fuel combustion. That matters.
Practical plant assessments focus on more than reactor size. Operators check feedstock moisture, particle consistency, oxygen sealing, and heating response. A well-tuned twin-screw line may deliver steady material movement, while a rotary kiln can tolerate wider feed variation. Fluidized beds offer strong heat transfer but need careful dust control. Microwave systems can heat uneven feedstock quickly, although maintenance costs may be underestimated. Induction heating responds fast, yet metal contamination can create operational problems.
A reliable electric plant needs accurate thermocouples, insulated reactor walls, automated pressure control, and dependable condensers. Control software should record temperature changes every few seconds. Small leaks can disturb gas quality. Poor feed preparation can cause blockages. The output may include recovered oil, non-condensable gas, and solid char, depending on the approved feedstock and process settings. Electricity demand remains a serious issue, especially during startup and cold weather. Renewable power can reduce emissions, but grid stability still matters. Some performance claims look impressive on paper. Real production data may tell a less comfortable story.
Performance, Sustainability, and Commercial Applications
Fully electric continuous pyrolysis plants are judged by more than headline output. Their value appears in stable throughput, controlled heating, and predictable product quality. Electric reactors can respond quickly to temperature changes, especially when feedstock moisture varies. That response supports continuous operation, but it does not remove preparation requirements. Operators still need sorting, drying, and steady particle sizing. Small errors become expensive.
Performance should be measured with site data, not brochure estimates. Useful indicators include tonnes processed per hour, electricity consumption, carbon intensity, uptime, and maintenance intervals. Independent laboratory testing can verify recovered carbon, liquid fractions, and process gas quality. Renewable electricity can lower operational emissions, although grid intensity changes by location and season. Heat recovery may reduce demand further, but insulation losses and start-up energy deserve honest accounting. The numbers matter.
Commercial applications depend on consistent outlets. Processed agricultural residues may support soil amendments or industrial carbon products, subject to testing and local approval. Recovered oils can serve as industrial feedstock when specifications, storage systems, and regulations align. Some facilities may process sorted end-of-life materials under controlled conditions. Continuous designs can reduce labor per tonne and improve scheduling for medium and large sites. However, economics remain sensitive to electricity prices, feedstock contracts, product buyers, and unexpected downtime. Real-world variability remains. A responsible feasibility study should include third-party verification, operator training, emergency controls, and conservative production estimates.
| Rank | Plant Profile | Primary Feedstock | Typical Continuous Capacity | Operating Temperature | Electric Heating Requirement | Main Product Yield | Energy Self-Sufficiency Potential | Environmental Performance | Best-Fit Commercial Applications |
|---|---|---|---|---|---|---|---|---|---|
| 1 | Electric Waste-Tire Pyrolysis Plant High resource recovery | End-of-life tires, rubber products | 2–5 t/h | 450–550°C | 0.7–1.2 MWh/t of feed | Pyrolysis oil: 35–45%; recovered carbonaceous char: 30–40%; non-condensable gas: 10–15%; recovered steel: 10–15% | Usually high after start-up when non-condensable gas is cleaned and recirculated; external electricity remains necessary for drives and controls. | Potentially avoids open burning and landfill disposal; requires sulfur, particulate, and volatile-organic-compound controls. | Recovered fuel oil, carbon-black substitute, steel recycling, rubber and asphalt modifiers. |
| 2 | Electric Mixed-Plastic Pyrolysis Plant High liquid-product yield | Polyolefin-rich plastic waste such as PE and PP | 5–10 t/h | 450–550°C | 0.4–0.8 MWh/t of feed | Condensable oil and wax: 65–80%; gas: 10–20%; solid residue: generally below 10% when feed is properly sorted. | Good potential because product gas can supply part of the process heat after cleaning; sorting and pretreatment consume additional electricity. | Can reduce demand for virgin petrochemical feedstock; chlorine, nitrogen, metals, and additives must be controlled. | Plastic-to-feedstock projects, wax production, chemical recycling, and industrial fuel production. |
| 3 | Electric Biomass Fast-Pyrolysis Plant Renewable carbon platform | Wood residues, forestry by-products, clean agricultural biomass | 1–3 t/h | 450–600°C | 0.8–1.5 MWh/t of dry feed | Bio-oil: 35–55%; biochar: 20–35%; permanent and non-condensable gas: 10–20%; remaining fraction is moisture and process loss. | Moderate to high when process gas and a portion of biochar are used for heat; feed drying can be the largest energy load. | Can provide renewable carbon storage through stable biochar; sustainability depends on residue sourcing and moisture management. | Renewable liquid fuels, soil-amendment biochar, carbon-removal projects, and biomass-derived chemicals. |
| 4 | Electric Sewage-Sludge Pyrolysis Plant Waste-risk reduction | Dried municipal sewage sludge and biosolids | 0.5–2 t/h | 450–650°C | 0.9–1.6 MWh/t of dry feed | Mineral-rich biochar: 35–50%; condensable products: 15–30%; gas: 10–20%; yield varies considerably with ash and moisture content. | Limited to moderate because drying requires substantial heat; heat recovery from hot char and product gas is essential. | Reduces pathogen and odor risks and concentrates minerals; heavy metals and contaminants must be tested before beneficial reuse. | Wastewater-treatment facilities, phosphorus recovery, fuel-gas production, and controlled soil or construction-material applications. |
| 5 | Electric Agricultural-Residue Pyrolysis Plant Distributed rural deployment | Rice husks, nut shells, corn residues, straw pellets, and other dry residues | 1–4 t/h | 400–600°C | 0.7–1.4 MWh/t of dry feed | Biochar: 25–40%; bio-oil: 25–45%; gas: 10–20%; actual yield depends on ash content, particle size, and residence time. | High potential for dry feedstocks when product gas is recirculated; low-moisture preparation is important for stable operation. | Can convert residues that are often burned in fields into usable products; air-quality benefits depend on feedstock collection and emission treatment. | Biochar production, decentralized heat and power, agricultural carbon projects, and renewable chemical intermediates. |
| 6 | Electric Refuse-Derived-Fuel Pyrolysis Plant Municipal waste diversion | Prepared refuse-derived fuel, textiles, paper-rich waste, and mixed dry residuals | 3–8 t/h | 450–650°C | 0.6–1.2 MWh/t of feed | Condensable hydrocarbons: 35–55%; solid char and inert fraction: 15–30%; gas: 10–20%; remaining material depends on ash content. | Moderate when the feed is dry and well prepared; high ash, moisture, and inert content reduce net energy performance. | May reduce landfill use and avoid direct combustion emissions; requires robust removal of chlorine, metals, dust, and acid gases. | Municipal waste diversion, industrial fuel production, recovered-carbon products, and waste-management hubs. |
| 7 | Electric Laminated-Plastic and Composite-Waste Plant Specialty recycling | Composite packaging, laminated films, coated textiles, and selected thermoset-rich residues | 0.5–3 t/h | 500–700°C | 0.9–1.8 MWh/t of feed | Condensable hydrocarbons: 25–50%; solid carbon and mineral residue: 25–45%; gas: 10–20%; composition is strongly feed-dependent. | Moderate; electric heating offers precise temperature control, while product-gas recovery can reduce operating electricity demand indirectly through heat recovery. | Enables treatment of difficult-to-recycle materials; fluorinated, chlorinated, brominated, and metal-containing components need dedicated controls. | Specialty polymer recovery, composite-material recycling, coated-fabric treatment, and production of controlled carbonaceous solids. |
Data note: The figures are engineering reference ranges compiled from commonly reported continuous pyrolysis operating conditions and material-balance ranges. Actual performance depends on feedstock composition, moisture, ash, particle size, reactor design, heat-recovery efficiency, product specifications, and emission-control systems. “Fully electric” refers to electrically supplied reactor heating; auxiliary equipment may still require additional electricity or external utilities.