contact-button

How to Choose a Battery Laser Welder in 2026

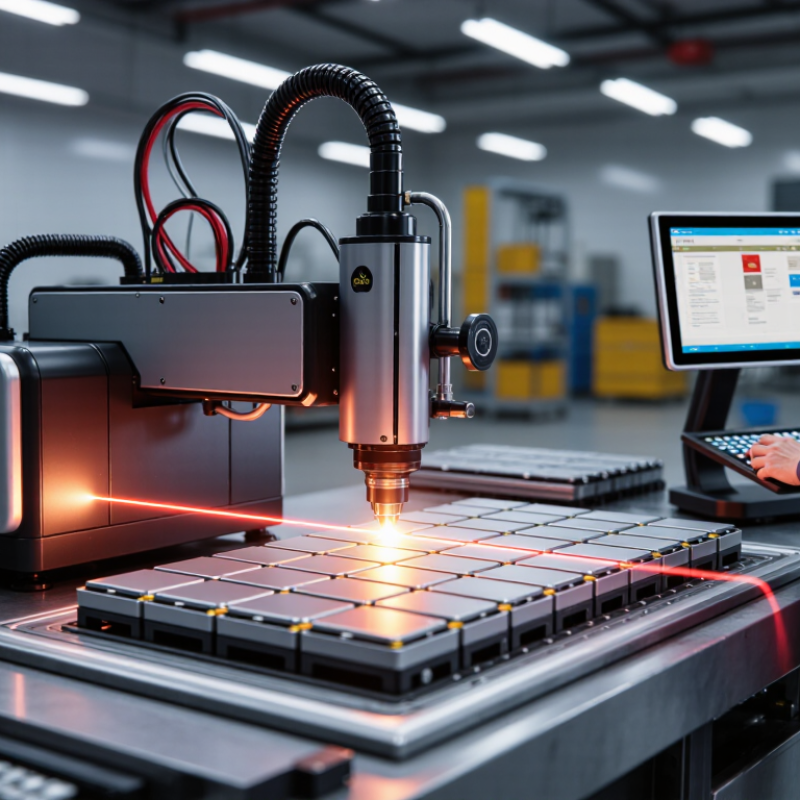
Choosing a Battery Laser Welder in 2026 means matching the machine to the cells, joints, and production conditions you actually use. A model built for thin nickel tabs may not suit thicker connectors or a different battery format. Start with the workpiece: identify its materials, dimensions, joint design, and required weld consistency. Then compare laser power, pulse control, positioning accuracy, and available fixtures. These details matter more than a headline specification.

Ask suppliers for documented technical data and sample welds using materials like yours. Inspect the joints under magnification, and check for consistent penetration, clean edges, and minimal heat impact. A neat surface can still hide a weak connection. It is an easy detail to overlook.

Also consider operator training, guarding, extraction, maintenance access, and service response. A fast machine can become a bottleneck if changeovers are awkward or replacement parts take weeks to arrive. Confirm that the system’s safety features and operating instructions fit your facility’s procedures. Have qualified personnel assess the setup before production begins.

There is no single best choice. That may be inconvenient, but it is honest. Compare total operating costs, not just purchase price, and run a realistic trial before committing. The right Battery Laser Welder should produce repeatable joints on your actual components, with settings your team can control and verify. A little uncertainty remains until the test parts are in hand.
How to Choose a Battery Laser Welder in 2026

Map Cell Format and Tab Metals: 18650 Cells Measure 18 × 65 mm

In 2026, choosing a battery laser welder begins with the cell and tab materials, not a headline power rating. An 18650 cell measures about 18 mm in diameter and 65 mm long. These are nominal dimensions; check the cell drawing and measure samples before designing a fixture. A few millimeters of positioning error can shift the weld away from the terminal.

Map each joint in the pack. Record whether the tab is nickel, nickel-plated steel, copper, or another specified material, and note its thickness. Metals respond differently to laser energy: reflective copper can be harder to couple energy into than nickel, while excess heat can damage nearby components. Do not assume a setting that works on one tab will transfer to another. It may not.

Fit the workholding around the cylindrical cell so it cannot roll, and keep the tab flat against the terminal. Small details matter. Ask for adjustable pulse energy, a stable focus, and repeatable positioning, then validate the process on representative coupons before production. Inspect weld consistency and test joint strength using a documented method. A neat-looking spot is not proof of a sound joint. Cell maker limits and pack design should guide heat input; this part deserves a second look.

Compare 1,070-nm IR and 450-nm Blue Lasers for Copper Tabs

When choosing a battery laser welder for copper tabs, compare how each wavelength couples with the metal. Copper reflects much of the near-infrared energy at 1,070 nm, especially before the surface begins to heat. This can make initial energy absorption less predictable. A 450-nm blue laser is generally absorbed more readily by copper, which can support stable weld formation at lower input energy.

Small details matter.

That advantage does not guarantee a better joint. Tab thickness, surface finish, clamping pressure, spot size, and travel speed all affect penetration and spatter. A practical comparison uses sample tabs matching the actual material stack, then checks weld consistency and cross-sections—not just appearance.

Not always.

The best wavelength depends on the job. IR systems may suit established processes and varied materials, while blue systems can be attractive for copper-heavy work. Consider pulse control, fixture access, maintenance, and operator training alongside wavelength. A neat bead can still hide weak fusion. If production conditions differ from the test setup, repeat the trials before settling on settings.

Set Power and Pulse Parameters Through Representative Coupon Welds

Battery-cell joints vary with tab thickness, surface films, and clamping pressure. The IEA’s Global EV Outlook 2024 reports that electric-vehicle battery demand exceeded 750 GWh in 2023, a 40% annual increase. That scale makes repeatable weld settings essential, but production speed should not set your first parameters.

Cut coupons from the same material lot as the intended parts. Match tab overlap, fixture pressure, and cleaning method; mark each sample. Start with low pulse energy, then change one variable at a time: power, pulse duration, or spacing. Keep a simple log. Inspect the bead, peel the joint, and record failure location and pull force. The U.S. Department of Energy’s 2023 National Blueprint for Lithium Batteries highlights manufacturing quality and yield as priorities; coupon tests connect those goals to measurable shop-floor evidence. A shiny bead can still hide weak fusion. I would not trust appearance alone.

Compare settings across several coupons, not one lucky weld. Check for burn-through, spatter, distortion, and inconsistent peel results. Then test the best window at the edges, not just the center. A slight wobble in fixture pressure can change the outcome. That is worth admitting. Set production limits only after repeatability checks, and revisit them when material, optics, or fixturing changes.

Qualify Aluminum Joints Against ISO 13919-2 Weld-Quality Levels

How to Choose a Battery Laser Welder in 2026
Qualify Aluminum Joints Against ISO 13919-2 Weld-Quality Levels

For battery components, a neat aluminum weld is not enough. ISO 13919-2 defines quality levels for imperfections in laser and electron-beam welds in aluminum and its alloys. Levels B, C, and D set different acceptance limits, with B generally the most stringent. Confirm the applicable edition and project requirements before selecting a target. The standard does not replace engineering decisions about joint strength or service conditions.

Tips: Test representative coupons. Match the alloy, thickness, joint fit-up, and surface condition. Check for porosity, cracks, undercut, and incomplete penetration using inspection methods suited to the part. Keep records of settings and results. Small gaps can matter.

When comparing a battery laser welder, look for stable energy control, repeatable positioning, and settings that can be locked and recorded. Then qualify the process across its intended operating range, not just on one ideal sample. A bright bead can still conceal internal defects. I would not treat one passing coupon as proof; real production variation deserves attention, even when it complicates the schedule.

How to Choose a Battery Laser Welder in 2026

ISO 13919-2:2021 aluminum weld-quality levels, ranked by acceptance stringency

How to read this: Level B is the most stringent, followed by C and D. The bars show only this ordinal ranking—not numerical defect limits or a certified weld score. When selecting a welder, confirm that its process can consistently produce joints meeting the quality level required for your application, then qualify the joint against the standard’s applicable criteria.

Require Class 4 Laser Controls Under IEC 60825-1 Safety Requirements

How to Choose a Battery Laser Welder in 2026: Require Class 4 Laser Controls Under IEC 60825-1 Safety Requirements

When comparing battery laser welders, check the safety design before focusing on speed or footprint. Ask whether the beam path is enclosed, access doors are interlocked, and a suitable beam stop is fitted. IEC 60825-1:2014, including Amendment 1:2021, provides requirements for laser classification and product safety. Class 4 beams can injure eyes and skin, including through hazardous reflections. Containment matters.

Look for clear Class 4 labels, an emergency stop, and controlled access during operation. Select protective eyewear for the laser’s actual wavelength and exposure conditions; a generic pair is not enough. The risk assessment should also address setup, maintenance, and unexpected access. Small details matter. A door interlock that is easy to bypass deserves a closer review.

OSHA estimates that about 2,000 U.S. workers experience job-related eye injuries requiring medical treatment each day. This figure covers workplace eye injuries generally, not laser incidents specifically, but it underlines why protection cannot be an afterthought. Ask the supplier for the laser classification, safety documentation, and operator-training materials. I would verify these details on the actual machine, not rely only on a brochure.

How to Choose a Battery Laser Welder in 2026 — Require Class 4 Laser Controls Under IEC 60825-1 Safety Requirements

Selection Dimension What to Specify or Verify Why It Matters Evidence to Request
Laser product classification Confirm the accessible-emission classification and applicable IEC 60825-1 edition for the product and the destination market. Treat an explicitly Class 4 system as a high-hazard laser installation. Class 4 beams can cause serious eye and skin injury; hazardous reflections may also need assessment. Classification depends on accessible emission, not simply the laser’s stated output power. Product classification report, safety documentation, and confirmation of the standards and local regulatory requirements applied.
Enclosure and access control For enclosed operation, inspect the beam enclosure, access panels, viewing windows, and any interlocks. Verify that access during emission is controlled and that interlocks act as intended. An enclosure can reduce exposure only when its construction and safety functions are suitable for the actual laser, wavelength, and operating conditions. Enclosure drawings, interlock function test, window specifications, and documented risk assessment.
Class 4 operating mode If the beam is accessible during setup or operation, require a site-specific laser safety program, controlled access, suitable beam termination, warning indicators, and an emergency-stop strategy. Class 4 controls must address the real installation and work practices. Protective measures should be selected through risk assessment and applicable rules, rather than assumed from a generic checklist. Laser safety procedures, access-control plan, emergency-stop test results, and appointed safety responsibilities.
Wavelength and optical safety Record the emitted wavelength or wavelengths and pulse or continuous-wave operating modes. Select wavelength-appropriate protective eyewear based on a documented optical-density and exposure assessment. Laser eyewear is not interchangeable across wavelengths or operating conditions. Enclosure windows and sensors also need suitable specifications for the emitted radiation. Laser source specification, eyewear marking and assessment, and window or filter transmission data.
Laser power and operating mode Match continuous-wave or pulsed output, pulse energy, pulse duration, repetition rate, and available power range to the joint design and process trials. Do not select on maximum power alone. Weld penetration, heat input, spatter, and risk of damaging thin battery materials depend on the combined process parameters and joint geometry. Verified output specifications, parameter ranges, and trial-weld results on representative materials and parts.
Battery materials and joint types Test the actual material combinations and thicknesses, such as copper-to-copper, aluminum-to-aluminum, or dissimilar-metal joints where applicable. Include the production joint geometry. Reflectivity, thermal conductivity, surface condition, and dissimilar-metal behavior affect process stability and weld quality. Results on one material pair do not establish performance on another. Sample welds, cross-sections, applicable mechanical or electrical test results, and documented acceptance criteria.
Beam delivery and positioning Check working distance, focus adjustment, spot-size range, scanning or motion system, fixture access, and repeatability at the intended production location. Reliable positioning and consistent focus help maintain weld quality across cell tabs, busbars, and other battery assemblies. Layout drawings, positioning specifications, repeatability data, and an application trial.
Weld monitoring and traceability Consider process monitoring for relevant signals, such as reflected light or thermal emissions, and record process settings against part or batch identifiers where required. Monitoring can help identify process variation, but it does not by itself prove weld integrity. Validation still requires appropriate inspection and testing. Monitoring description, data-export example, validation plan, and inspection method.
Fume and process contamination Assess extraction and filtration for fumes and particles generated by the specific materials, coatings, and process. Position extraction so it does not interfere with the weld. Laser processing can generate airborne contaminants; suitable controls depend on the work material and local occupational-health requirements. Material-specific risk assessment, extraction airflow information, filter details, and maintenance instructions.
Production integration and support Verify utilities, cycle-time capability, fixture changes, maintenance access, training, spare-parts availability, and service response for the intended production volume. A system that meets weld requirements in a trial may still be unsuitable if it cannot meet production, uptime, or maintenance needs. Factory acceptance criteria, cycle-time trial, maintenance schedule, operator training plan, and service terms.

Safety note: IEC 60825-1 addresses laser product classification and related safety requirements. Confirm the edition adopted in the destination market and have a qualified laser safety professional assess the complete installation. This table is a selection guide, not a substitute for a formal risk assessment or compliance review.