

Design and development by Raincastle Communications.

Finding a reliable Precision Cnc Parts supplier takes more than comparing unit prices. A polished website cannot confirm that a shop will hold a tight tolerance across a production run. Look for evidence: recent inspection reports, documented material grades, calibrated measurement tools, and clear process controls. Ask how the supplier checks a critical bore or flatness requirement, not just whether it can meet the drawing. Details matter.
A useful evaluation starts with your actual part, drawing, material, finish, and expected order volume. Request a quotation that identifies assumptions, tolerances, lead time, and any proposed design changes. If practical, begin with sample parts and compare measured results against the drawing. Check whether inspection records identify the equipment and measurement method; a number without context is harder to trust. Also notice how quickly questions are answered, especially when specifications are unclear. Communication is part of quality.
Supplier audits, customer references, and certifications can add confidence, but none guarantees a perfect outcome. Their value depends on scope and current practices. A certificate may cover one site or process, while your part uses another. Ask for relevant evidence and verify what it actually demonstrates. No checklist is foolproof. Even experienced buyers can miss a detail, such as a hidden finish requirement or a tolerance that raises cost without improving function. That is worth revisiting. A dependable supplier should explain risks plainly, flag inconsistencies before machining, and agree on how changes will be approved. The aim is not simply to find a low quote. It is to build a repeatable process that delivers conforming parts, realistic lead times, and records you can review when something does not go to plan.
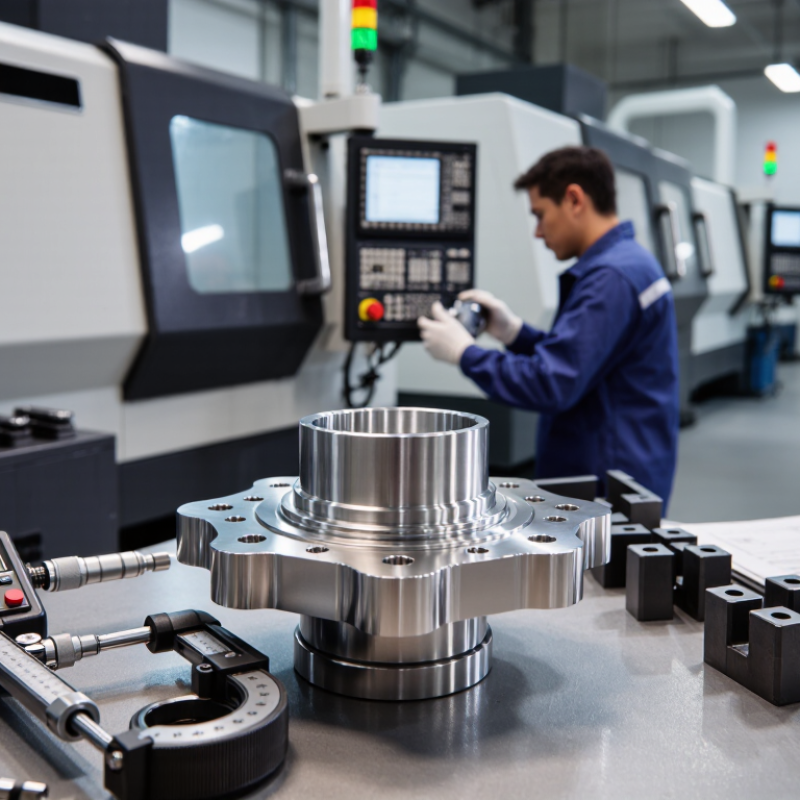
A reliable CNC supplier should receive a drawing that defines both size limits and geometric relationships. ISO 286-2 gives the tolerance values for common nominal sizes and IT grades. For a 25 mm hole, the ISO 286-2 H7 limits are 25.000–25.021 mm, a 21 μm tolerance zone. That is useful only when the fit and function justify it. Specifying H7 everywhere can raise machining and inspection costs without improving performance.
GD&T adds controls that size limits cannot express. ASME Y14.5 defines symbols for features such as position, flatness, and perpendicularity. For a mounting plate, a position tolerance tied to clear datums can clarify how hole locations relate to the mating assembly. Ask suppliers how they will inspect each critical feature, and request measurement records for high-risk dimensions. NIST’s Engineering Statistics Handbook also explains why measurement variation matters: a result near a specification limit needs uncertainty considered, not just a pass/fail reading. Real shop conditions can complicate this; revisit tolerances after reviewing prototype measurements.
Tips: Mark functional dimensions clearly. Name datum surfaces. Use tighter tolerances only where assembly or function requires them. Before release, compare the drawing with the inspection plan.
| Part Feature | Example Requirement | ISO 286 Size Tolerance | GD&T Requirement | Inspection Method | Supplier Evidence to Request |
|---|---|---|---|---|---|
| Bearing-seat bore in an aluminum housing | Ø25 mm; bearing seat length 18 mm | Ø25 H7; specify limits using the applicable ISO 286 table and standard edition | Position of the bore axis: ⌀0.03 mm relative to datums A and B | Calibrated bore gauge or air gauge; CMM for position | First-article inspection report listing measured bore size and positional deviation |
| Mating steel shaft bearing seat | Ø25 mm; surface finish Ra 0.8 µm where required by the drawing | Ø25 g6; confirm the shaft limits against the applicable ISO 286 table | Total runout 0.02 mm to datum axis A | Outside micrometer; roundness or runout measurement on a suitable fixture | Recorded shaft measurements, calibration status, and material certificate when specified |
| Dowel-pin locating hole | Ø8 mm through hole in a machined plate | Ø8 H7; use the ISO 286 limits for the stated nominal size | Position: ⌀0.05 mm relative to datums A, B, and C | Plug gauge for size; CMM or coordinate inspection for position | Inspection results tied to the drawing datum scheme, not size readings alone |
| Ground locating shaft | Ø10 mm nominal; functional sliding-fit surface | Ø10 h6; confirm limits and fit suitability for the mating feature | Cylindricity 0.01 mm on the indicated functional surface | Micrometer; roundness or cylindricity instrument for geometric verification | Documented inspection method and results for both size and form |
| Flat mounting face | Machined face, 40 × 30 mm | Apply the drawing’s general linear tolerance unless a specific size tolerance is shown | Flatness 0.05 mm; perpendicularity 0.05 mm to datum A for the indicated side face | Surface plate and indicator, or CMM with an agreed alignment method | Inspection report identifying the datum setup and the measured geometric deviations |
| Threaded mounting hole pattern | Four M6 × 1 tapped holes on a 40 × 30 mm pattern | Thread tolerance class 6H unless the drawing specifies otherwise; ISO 286 does not define thread classes | Position: ⌀0.10 mm at MMC relative to datums A, B, and C, if permitted by the drawing standard | Thread plug gauges; CMM or dedicated pattern inspection fixture | Thread-gauge results and true-position results reported against the specified datum reference frame |
| Supplier quality-system and process review | Confirm capability for the material, quantity, finish, and tolerance level in the RFQ | Ask how ISO 286 fits are interpreted, programmed, and checked at the required nominal sizes | Verify that the supplier can interpret the selected GD&T standard and datum scheme consistently | Review sample reports, measurement equipment, and control plans | Request a first-article report, equipment calibration records, nonconformance process, and inspection plan |
Specification note: ISO 286 tolerance grades and deviations depend on nominal size and the selected tolerance position. State the drawing standard and edition, units, datums, material, surface-finish requirements, and any general tolerances. Apply one GD&T standard consistently, such as ISO 1101, and have the supplier confirm interpretation before production.
Design and development by Raincastle Communications.
 Customer Support
 Request Sample
 Contact