2026 Top Aluminium Tri Fold Blind Rivets for Composites
Choosing the right fastener for composite panels is rarely a simple catalogue decision. Aluminium Tri-Fold Blind Rivets For Composite Materials offer broad load distribution behind fragile skins. Their three-legged expansion can reduce pull-through risk when access is available from one side only. This matters in sandwich panels, fiberglass enclosures, lightweight vehicle bodies, and interior structures.
Composite fastening specialist Dr. Stephen W. Tsai has emphasized, “Composite design is not simply metal design with different materials.” That principle guides this 2026 review. Rivet selection must consider laminate thickness, core density, hole quality, grip range, and washer support. Aluminium provides low weight and useful corrosion resistance. However, it may not suit every galvanic environment. Sealants, coatings, and isolation layers can change the result.
Small details matter.
A clean hole protects the laminate. Correct clamping prevents crushing. Controlled installation reduces uneven expansion. The rivet should fill the hole without forcing excessive pressure into the panel. Laboratory data helps, but field conditions can be less polite. Temperature changes, vibration, moisture, and hidden voids may weaken an otherwise attractive joint. That is the uncomfortable part.
This guide compares leading aluminium tri-fold blind rivets for 2026 applications. It considers practical installation, head design, mandrel retention, corrosion behavior, and composite compatibility. Readers should still validate every choice through representative testing. No chart can replace a real trial. Even experienced engineers occasionally overlook washer placement or local skin damage. Careful inspection remains essential, especially where repair access is limited and failure would be costly.
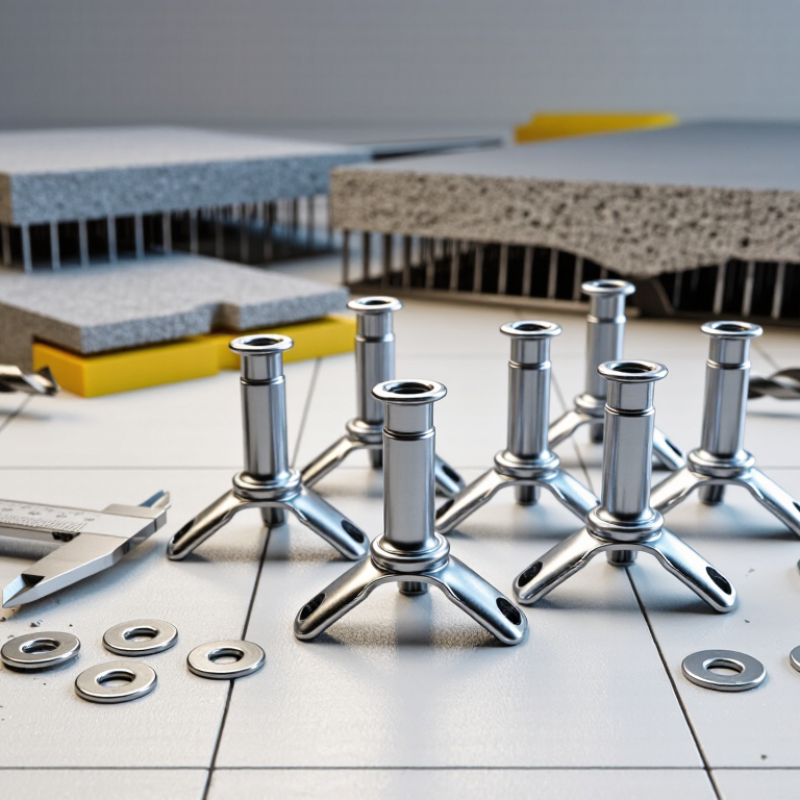
Table of Contents [Hide]
What Are Aluminium Tri-Fold Blind Rivets for Composite Materials?
Aluminium tri-fold blind rivets are fasteners designed for joining composite materials where access is available from one side. Their body expands into three broad legs behind the panel. This action spreads clamping pressure over a larger area than a standard blind rivet. It can reduce pull-through risks in thin laminates, honeycomb panels, and molded composite covers.
The aluminium body is lightweight and resists many forms of corrosion. However, it may not suit every environment. Contact with carbon-fiber composites can create galvanic corrosion when moisture enters the joint. A compatible coating, isolating washer, or barrier layer may be necessary. Hole accuracy also matters. Oversized holes can reduce grip, while excessive tightening may crush the laminate. In field repairs, technicians should inspect the panel thickness, rivet grip range, and rear-side expansion before installation. Small errors become expensive later.
Tips: Use a sharp, properly sized drill, and remove loose fibers around the hole. Choose a rivet with enough expansion space behind the panel. Test one fastener on scrap material first. This simple step often reveals unexpected crushing or poor setting. Do not judge strength by appearance alone. Check the joint under realistic vibration and load conditions, because composite behavior can be less predictable than metal.
How Tri-Fold Rivets Work in Composite Assemblies
2026 Top Aluminium Tri Fold Blind Rivets for Composites
How Tri-Fold Rivets Work in Composite Assemblies
Tri-fold blind rivets create a broad, three-point load pattern behind a composite panel. During installation, the mandrel pulls the rivet body through the drilled hole. The body then folds into three petals on the hidden side. These petals press against the rear surface. Load spreads across a wider area than with a standard blind rivet.
This action matters in thin laminates, honeycomb panels, and uneven rear access areas. A larger bearing area can reduce local pull-through risk. However, it does not replace proper laminate design. Hole diameter, grip range, and panel thickness must match the rivet specification. Excessive setting force may crush the laminate or damage the core. That failure can remain hidden.
Installation quality starts before the rivet enters the hole. Use a sharp, suitable drill and remove loose fibers around the opening. Clean dust from the hole without enlarging it. Aluminium may also require isolation from carbon fibers to limit galvanic corrosion. A compatible sleeve, coating, or barrier washer can help, depending on the assembly environment.
A practical inspection should check head seating, petal formation, and panel distortion. Small gaps deserve attention. They may indicate an incorrect grip length or poor hole preparation. The first installation is not always perfect. Test coupons and pull-out checks can reveal weaknesses before production begins. Composite assemblies reward patience, but field conditions still demand clear installation controls.
Key Performance Factors for Selecting Rivets in 2026
2026 Top Aluminium Tri Fold Blind Rivets for Composites
Selecting aluminium tri fold blind rivets for composite panels requires more than checking tensile strength. Grip range must match the combined panel thickness, including coatings, gaps, and local reinforcements. A rivet that is too short may not form its three legs fully. One that is too long can crush the laminate.
Key Performance Factors for Selecting Rivets in 2026
Corrosion compatibility deserves close attention. Aluminium rivets can react with carbon-fiber composites or nearby metal parts, especially in humid environments. Use suitable isolating layers and verify the assembly under realistic temperature and moisture cycles. Rivet head diameter also matters. A wider head spreads pressure across fragile skins, while excessive force may cause delamination. Hole quality is easy to underestimate. Clean, round holes improve folding consistency and reduce installation variation.
Tips: Confirm the actual grip range. Test the joint.
In field evaluations, vibration resistance and mandrel retention often separate reliable joints from disappointing ones. Check whether the folded rivet remains stable after repeated loading. Pull-out tests, shear tests, and visual inspections should support the selection, not replace engineering judgment. Installation tools must provide consistent stroke and nosepiece alignment. Small setup errors can create large performance differences. A perfect datasheet cannot predict every laminate behavior. That is why prototype testing remains necessary, even with familiar materials. Temperature exposure should also be measured, since resin systems and aluminium expand differently. Record failures honestly; they often reveal the real design limits.
2026 Top Aluminium Tri Fold Blind Rivets for Composites
Key Performance Factors for Selecting Rivets in 2026
Thermal expansion compatibility is a critical screening factor when aluminium tri-fold blind rivets are used with composite laminates. Aluminium alloys typically expand at approximately 23.6 µm/m·°C, while glass-fibre composites commonly range from 6 to 12 µm/m·°C and carbon-fibre composites from 0 to 2 µm/m·°C in the fibre direction. These differences should be evaluated together with grip range, hole quality, bearing strength, pull-through resistance, corrosion isolation, and joint load requirements.
Reference values are representative engineering ranges and may vary with laminate architecture, fibre orientation, resin system, alloy temper, and test direction. Final rivet selection should be verified against project-specific joint tests and applicable aerospace or structural fastening requirements.
Installation Steps for Aluminium Tri-Fold Blind Rivets
2026 Top Aluminium Tri Fold Blind Rivets for Composites
Installation Steps for Aluminium Tri-Fold Blind Rivets
Choose a rivet with the correct grip range for the composite panel and support structure. Measure both layers, including coatings and washers. Drill a clean hole with minimal pressure. A sharp drill reduces delamination around the entry point. Remove dust and inspect the hole edge. The U.S. Department of Energy reports that a 10% vehicle weight reduction can improve fuel economy by roughly 6–8%. Aluminium tri-fold rivets support this lightweight design goal, but only when installed correctly.
Insert the rivet body through the assembly until the flange sits flat. Keep the tool aligned with the hole. Pull the mandrel slowly until the three legs expand behind the panel. Stop when the flange is seated firmly. Do not over-compress the composite. Excess pressure can create hidden cracks. Release the mandrel and check that the legs formed evenly. A slight gap means the grip range may be wrong. Remove sharp mandrel remnants and inspect the joint visually.
Tips: Use a backing washer when the composite surface feels soft. Isolate aluminium from carbon-fibre layers to reduce galvanic corrosion. Record hole size, rivet length, and setting results. ISO fastener guidance and ASTM composite testing practices both emphasize repeatable preparation and inspection. I would not trust appearance alone. Tap lightly around the joint and check for movement. That simple check can reveal an installation mistake early.
2026 Top Aluminium Tri Fold Blind Rivets for Composites - Installation Steps for Aluminium Tri-Fold Blind Rivets
Selection guide and practical installation workflow for composite panels, covers, enclosures, and lightweight assemblies
| Configuration / Use Case | Typical Rivet Size | Typical Grip Range | Typical Hole Diameter | Recommended Features | Key Selection Considerations |
|---|---|---|---|---|---|
| Light composite panels | 3.2 mm diameter Aluminium body with steel mandrel | Approx. 1.0–3.0 mm | Approx. 3.3–3.4 mm | Large flange; low setting load; corrosion-compatible washer where required | Suitable for thin laminates and covers when the combined material thickness is within the stated grip range. |
| General composite-to-metal joints | 4.0 mm diameter Aluminium body with steel mandrel | Approx. 1.0–4.0 mm | Approx. 4.1–4.2 mm | Tri-fold expansion; wide load distribution; dome or large-flange head | A common starting configuration for medium-duty composite assemblies. Confirm the supplier’s actual grip chart before ordering. |
| Thicker sandwich panels | 4.8 mm diameter Aluminium body with steel mandrel | Approx. 3.0–6.0 mm | Approx. 4.9–5.0 mm | Large flange; extended grip option; controlled setting stroke | Use only when the rivet’s grip range covers the total clamped thickness, including skins, adhesive layers, and washers. |
| Soft-core or honeycomb composite panels | 4.0–4.8 mm diameter Large-flange tri-fold rivet | Selected according to actual panel thickness | As specified for the selected rivet diameter | Large bearing head; backing washer when permitted; low-distortion setting | Avoid excessive clamp force. The folded legs should spread behind the panel without crushing the core or damaging the laminate. |
| Outdoor or humid environments | Aluminium body with compatible mandrel material | According to the selected diameter and length | According to the selected diameter | Sealed or closed-end design where fluid ingress matters; compatible washer or coating | Check galvanic compatibility between the rivet, mandrel, fastened material, and any protective coating. Isolate dissimilar metals when necessary. |
| Access-limited assemblies | Open-end tri-fold blind rivet | According to the manufacturer’s grip table | Accurately drilled nominal hole | One-sided installation; mandrel retention if loose mandrels are unacceptable | Blind rivets are useful when the rear side is inaccessible, but the rear side still needs sufficient clearance for the folded legs. |
| Step | Installation Action | Technical Requirement | Inspection Check |
|---|---|---|---|
| 1. Confirm the joint design | Identify the composite type, laminate thickness, core structure, mating material, and access conditions. | Verify that the joint can tolerate drilling, clamping, and local bearing loads. | Check for adequate edge distance, access behind the panel, and clearance for the folded rivet legs. |
| 2. Measure the total grip thickness | Add the thicknesses of all sheets, skins, washers, spacers, and approved shims being clamped. | Select a rivet whose published grip range includes the measured total thickness. | Do not use a rivet that is too short, too long, or outside the stated grip range. |
| 3. Select the head style | Choose a large-flange head for soft, brittle, thin, or sandwich composite surfaces. | The head should distribute bearing pressure without breaking the laminate or crushing the skin. | Confirm that the head diameter does not interfere with adjacent parts or required clearances. |
| 4. Mark and support the work | Mark the hole location and support the panel close to the drilling point. | Prevent panel flexing, delamination, and local core collapse during drilling. | Ensure the marked hole is clear of edges, corners, existing fasteners, and damaged laminate. |
| 5. Drill the hole | Drill a round hole using a sharp, suitable bit at a controlled feed rate. | Use the hole diameter specified for the selected rivet; avoid oversize or oval holes. | Remove loose fibers and inspect for delamination, breakout, resin cracking, or crushed core. |
| 6. Deburr and clean | Lightly remove burrs without enlarging the hole, then clean away dust and chips. | The mating surfaces must sit flush, and debris must not prevent full rivet insertion. | Check that the rivet body passes through the joint without binding. |
| 7. Insert the rivet | Place the rivet through the joint from the accessible side until the flange contacts the outer surface. | The rivet body must pass through all layers, with the correct amount of body extending behind the joint. | Verify that the flange is seated flat and the mandrel is aligned with the rivet axis. |
| 8. Set the rivet | Fit the correct nosepiece and operate the hand, battery, or pneumatic rivet tool in line with the rivet. | Pull the mandrel smoothly until the tri-fold legs form and clamp the joint. | Stop when the mandrel head reaches the designed break point; do not over-stroke the tool. |
| 9. Inspect the formed legs | Examine the rear side when accessible, or use a suitable inspection method for blind locations. | The legs should be evenly formed and should bear against the rear surface without cutting into the panel. | Reject rivets with incomplete folding, tilted heads, spinning bodies, cracked laminate, or excessive crushing. |
| 10. Verify the finished joint | Check head seating, joint tightness, surface damage, and mandrel retention requirements. | The assembly should meet the design requirements for clamp force, shear, vibration, and environmental exposure. | Record the rivet type, diameter, grip range, tool setting, and inspection result for production traceability. |
Important: Dimensions and grip ranges shown above are typical selection examples rather than universal specifications. Actual hole diameter, grip range, mandrel material, head diameter, setting force, and load capacity vary by rivet design. Always use the selected rivet supplier’s current technical datasheet and validate the joint with representative composite materials before production use.
Common Applications, Benefits, and Limitations in Composites
2026 Top Aluminium Tri Fold Blind Rivets for Composites
Aluminium tri-fold blind rivets suit composite panels where only one side is reachable. Their three-legged expansion spreads clamping force across a wider area. This helps reduce local pull-through in thin fiberglass or carbon-fiber laminates. They appear in trailer walls, aircraft interiors, marine compartments, battery covers, and lightweight equipment enclosures.
Grand View Research valued the global composites market at about USD 95.8 billion in 2022, with continued growth expected through 2030. More composite assemblies mean more demand for controlled, repair-friendly fastening.
The U.S. Department of Energy reports that a 10% vehicle weight reduction can improve fuel economy by roughly 6% to 8%. Small fasteners matter when hundreds are installed.
Field experience shows several benefits. Aluminium offers low density, easy installation, and useful corrosion resistance in suitable environments. Tri-fold expansion can accommodate uneven or fragile surfaces better than standard blind rivets.
Still, they are not universal. Carbon fibers may accelerate galvanic corrosion against aluminium, especially with moisture and salt. Isolation washers, sealants, and compatible sleeves may be necessary.
Hole quality also matters; oversized holes can cause movement and laminate crushing. Some installers trust the wide expansion too much. That assumption fails under vibration.
Product datasheets, torque-free pull testing, edge-distance checks, and periodic inspection remain essential. Availability can also vary by diameter, grip range, and mandrel configuration.